Map the flow path
Locate drilling intersections and cleaning access.

CUSTOM PARTS / ENGINEERING & MACHINING
Cross-drilled passages, sealing faces and threaded connections need coordinated machining and cleaning. We develop the proposed stainless steel route around tool access, burr control and the features that seal or locate your assembly.
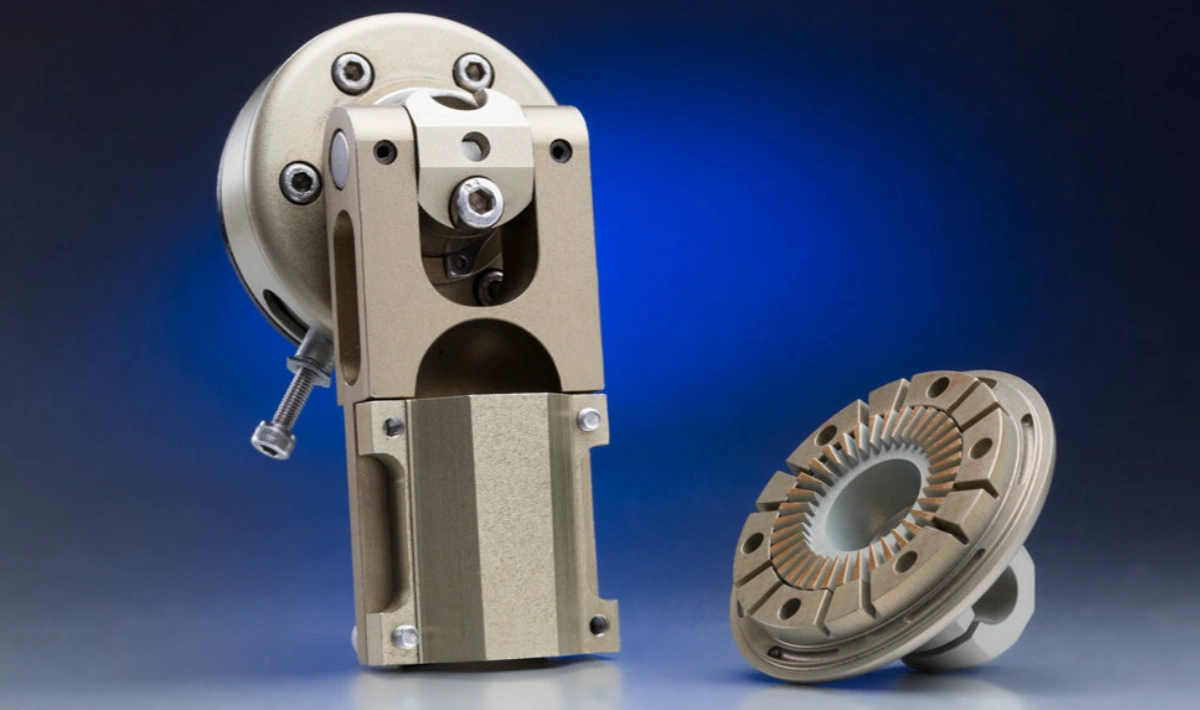
Our review links the feature that matters in your assembly to the proposed setup, machining sequence and acceptance check.
| Your part challenge | Our proposed approach | How to verify the result |
|---|---|---|
| Cross holes leave internal burrs | Plan drilling intersections and an accessible deburring route. | Define an inspection method for the internal intersections and passages. |
| A sealing face must survive handling | Separate sealing texture and edge requirements from appearance-only surfaces. | Check the defined face and protect it through cleaning and shipment. |
| Cutting becomes unstable | Review grade, rigidity, tool engagement and coolant delivery as a route. | Tie feature results to the tool and inspection checkpoints. |
ILLUSTRATIVE ENGINEERING BRIEF
Illustrative RFQ: 25 fluid blocks, an 80 × 50 × 25 mm body, Ø6 mm cross passages and a Ra 1.6 µm sealing-face requirement.
These numbers describe an example customer requirement, not a completed customer project or a guaranteed machining limit. Final feasibility is confirmed from the drawing.
An external dimensional report can miss burrs at intersecting passages. Surface texture alone also does not establish leak-tight performance.
Proposed acceptance: passage positions, specified face texture, internal burr acceptance and cleaning records. Functional pressure testing is a separately agreed scope.
Locate drilling intersections and cleaning access.
Review rigidity, engagement and grade-specific tool planning.
Identify sealing faces and the specified surface treatment.
Agree internal-burr and cleanliness checks alongside dimensions.
Confirm the grade after the functional requirements are clear.
Select the grade and condition for the actual corrosion, strength and joining requirements. A machinability preference does not automatically justify substituting 303 for 304 or 316L.
| Material option | Selection context | What to confirm |
|---|---|---|
| 303 | Machining-oriented components | Confirm corrosion and joining requirements. |
| 304 / 316L | Fluid and equipment components | Specify exposure, cleanliness and finishing needs. |
| 17-4PH | Strength-sensitive components | State the required condition and when final dimensions apply. |
Material reference: Material or fabrication reference ↗.
Provide a passage map and burr acceptance criteria. We can propose an access and inspection route for the intersections.
No. Passivation and leak testing address different requirements. State pressure, medium and acceptance criteria for any functional test.
Only with approved material substitution. Corrosion, joining and service requirements must still be met.
The example is a customer brief used to explain the proposed engineering route. Actual limits, cost and timing are confirmed from the complete drawing.
Send the CAD and drawing revision, exact grade, quantity and the critical requirements discussed above. Include mating-part details and required inspection records.
ENGINEER YOUR NEXT PART
Send the drawing and tell us which feature controls assembly, sealing or motion. Our review connects that requirement to a proposed route and inspection scope.