
Tooling and production, planned together
Metal stamping
services.
Clips, contacts and formed components for repeat orders. Bring tooling, material condition and inspection into the production plan from the start.
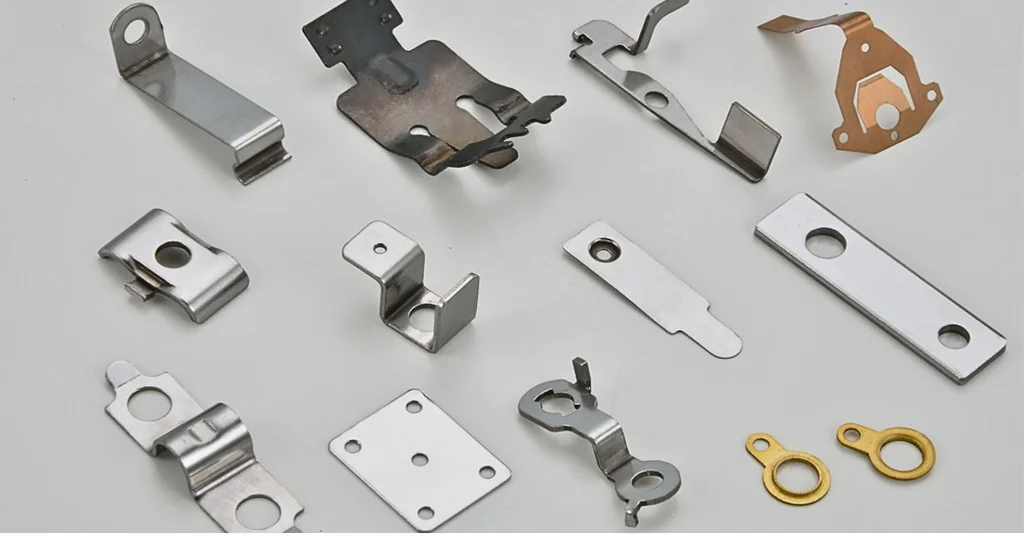
Tooling and material conditions govern the approved route. View dimensions, tolerances and conditions ↓
A stable part.
A planned production route.
Stamping combines dedicated tooling with repeated cutting and forming operations. The route makes sense when design stability, material behavior and demand support the investment.
What the service covers
- Separate tooling investment from the unit-part cost
- Define sample and first-article approval before repeat production
- Plan material condition, burr direction and final treatment together
Small features.
Real production decisions.
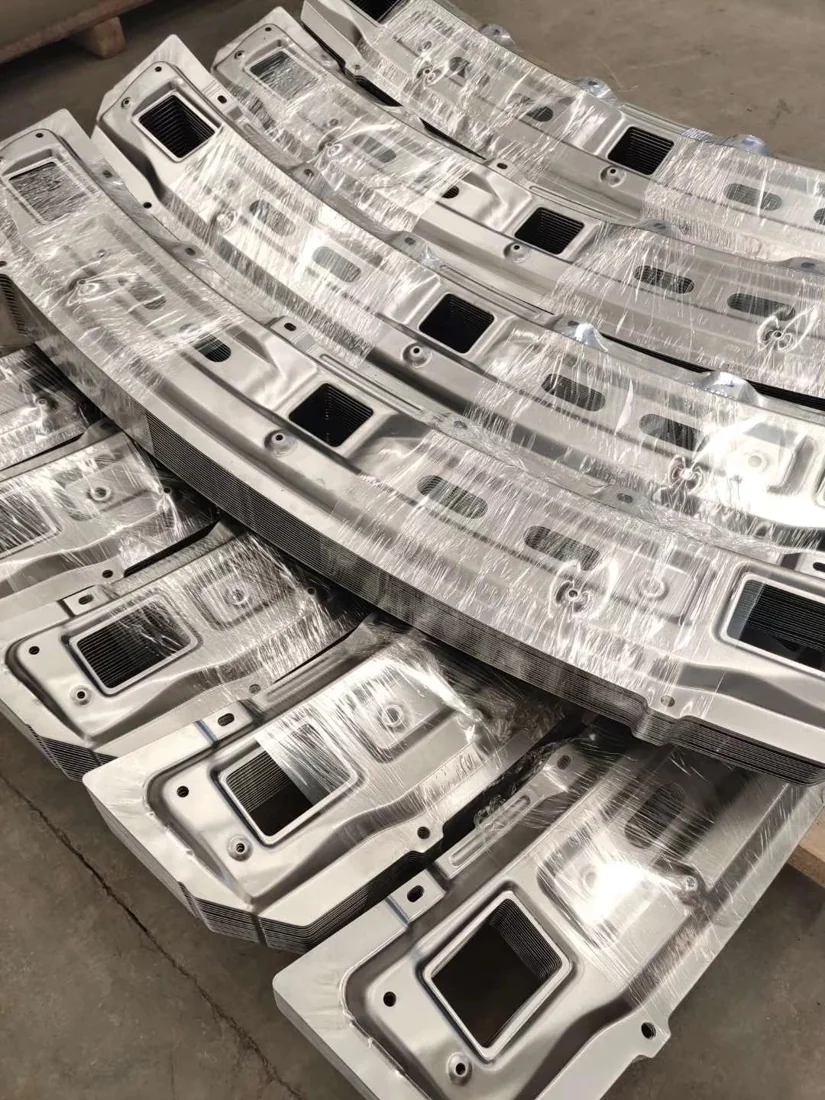
Clips, terminals and repeated formed panels need material condition, tooling and final acceptance to work together.
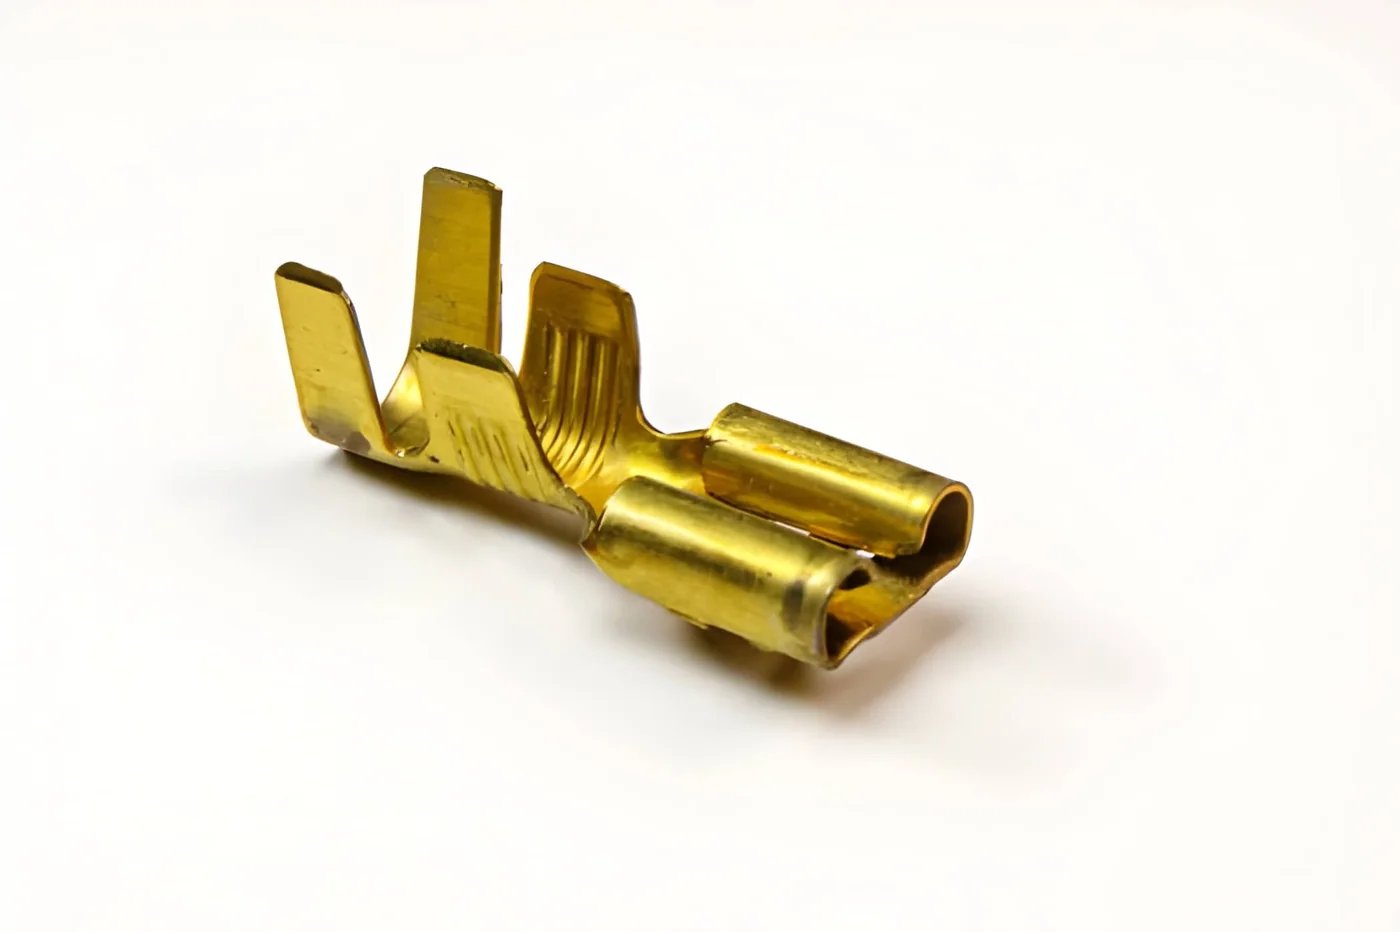
Formed terminals
Contact geometry, tabs and the surface that carries the function.
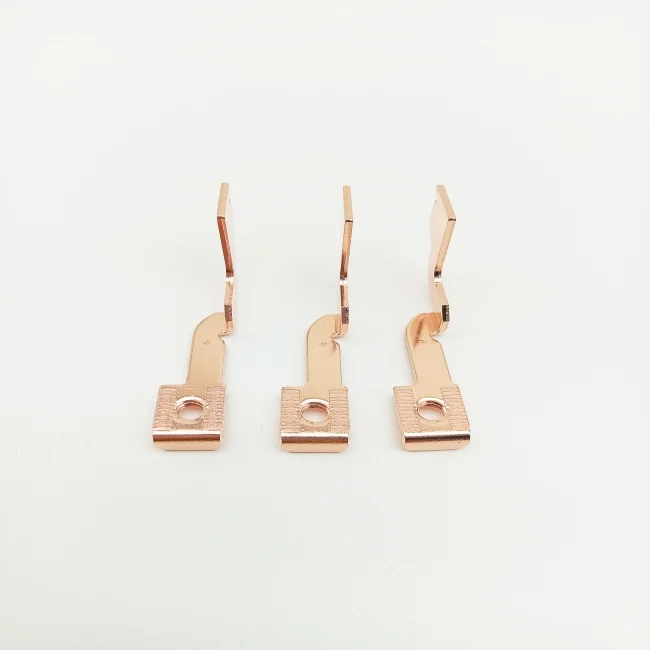
Contact tabs & connectors
Material condition, hole location and plating on the working surfaces.
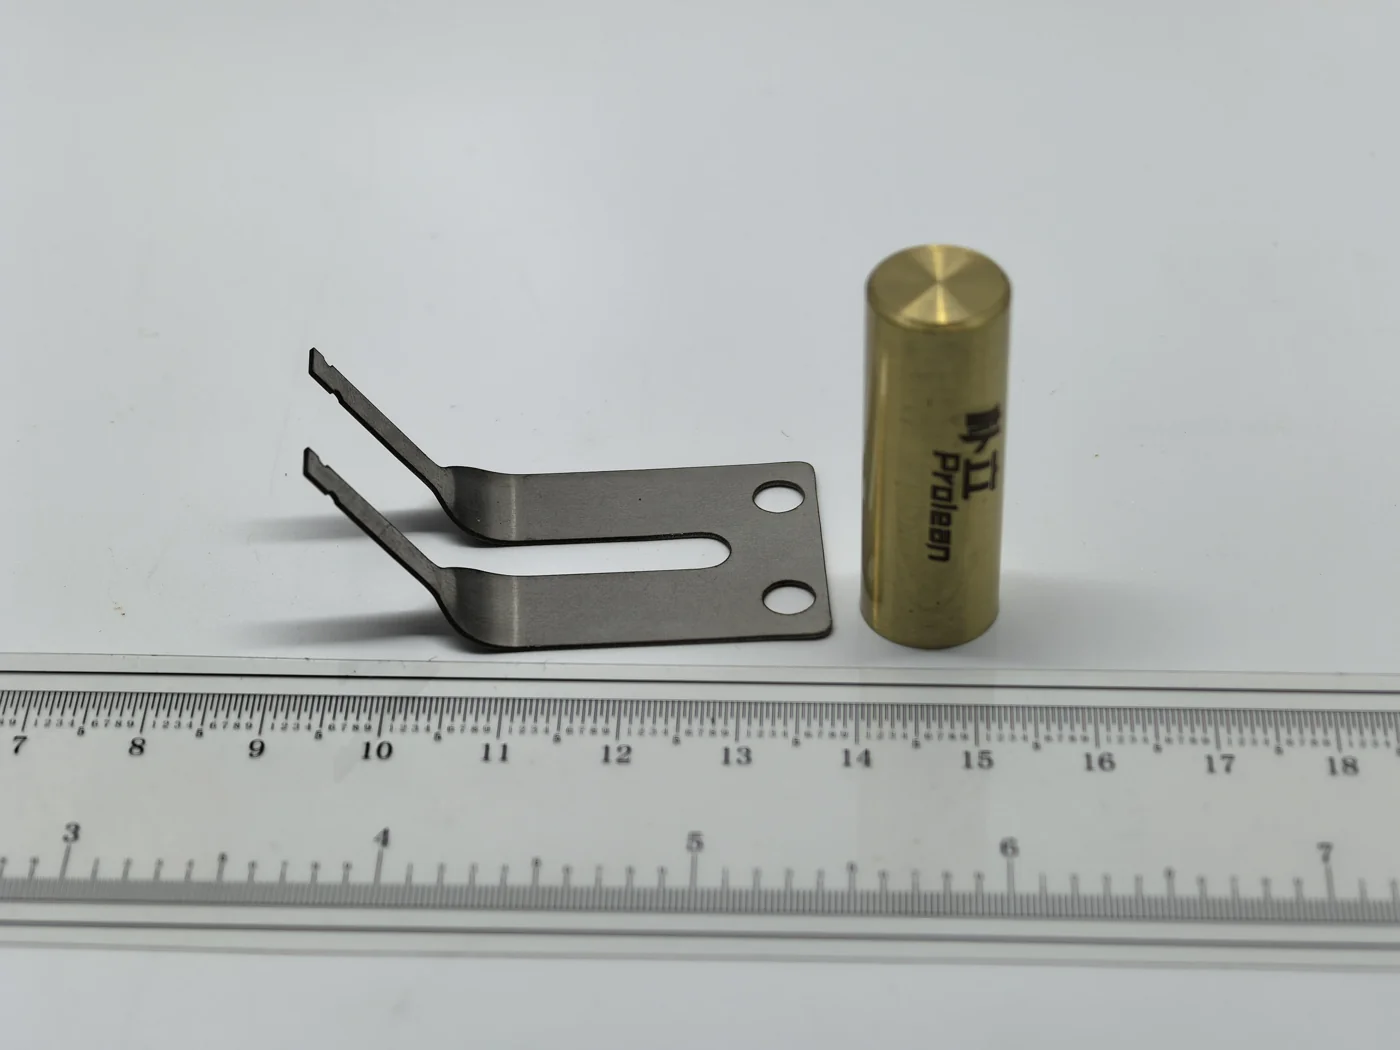
Spring clips
Free-state geometry, material temper and burr direction.
Repeated formed panels
Feature consistency, sample approval and protection between operations.
Plan tooling and repeat-part pricing together.
Share the design, tooling status, batch quantity and annual demand. Ask for tooling, first articles and production costs in one manufacturing scope.
CAD + material + thickness + quantityDefine the stock.
Then define the formed features.
Tooling decisions need more than a material name. Provide thickness, final geometry, critical fits and the material condition before the tool is designed.
| Material group | Specify in the RFQ | What determines the tooling route |
|---|---|---|
| Aluminum | Exact alloy and temper, sheet or strip thickness, grain direction and final treatment | Blank size, forming severity, radius, material flow and the required final geometry |
| Carbon and low-alloy steel | Grade, strength class, thickness tolerance, coating and supply condition | Required force, strip layout, operation sequence and critical feature relationships |
| Stainless steel | Exact grade and condition, thickness, surface finish and grain direction | Work hardening, springback, tooling access, radius and surface protection |
| Copper and brass alloys | Exact grade and temper, thickness, conductivity and contact-face requirements | Bend severity, elastic behavior, burr direction and plating sequence |
A dimensional brief the tooling team can use.
Example dimensions in mm. Specify thickness, hole size, inside radius, flange and datum separately, then add the actual functional tolerances.
- Thickness t
- 1.0 mm
- Hole
- Ø3.0 mm
- Inside radius
- R1.5 mm
- Outside height
- 8 mm
Drawing and execution standards
Make acceptance measurable: identify the standard, edition, class and the features it controls in the order documents.
| Requirement | Applicable standard | How it enters the order |
|---|---|---|
| General linear & angular dimensions | ISO 2768-1 | Select the tolerance class and applicable edition on the drawing. Individually toleranced features remain explicit. |
| Geometrical specification | ISO 22081 | Define the general geometrical requirement, datum system and applicable features. Specify numeric controls separately where function requires them. |
| Material purchasing specification | ASTM B209/B209M · ASTM A480/A480M | Aluminum sheet/plate and stainless sheet/strip requirements respectively. State alloy, temper, product form and the required document. |
The standard, edition and class stated in the accepted drawing and order define the requirements. The agreed inspection plan establishes how the finished part is checked.
Choose the route around the part and the demand.
Metal stamping uses a press and dedicated tooling to cut or form sheet and strip. Geometry, material behavior and repeat demand determine whether a die-based route makes sense.
| Route | Part characteristics | Selection criteria |
|---|---|---|
| Progressive die | A strip advances through piercing, blanking and forming stations. | Carrier layout, feed direction, feature sequence, scrap and stable repeat demand. |
| Transfer or separate operations | Individual blanks move between forming stages. | Handling, locating features, forming depth and the relationship between operations. |
| Drawing | A blank forms into a cup, shell or enclosure-like shape. | Material flow, corner radii, blank holding, thinning and any intermediate operations. |
| Multi-direction forming | Clips or small components need bends from several directions. | Tool access, spring behavior, sequence and whether a suitable tooling configuration is available. |
Select the route around the geometry, material condition and production demand. The quotation confirms tooling configuration, secondary operations and the manufacturing scope.
Plan the feature sequence before the tool.
Early design review connects the flat blank, forming stages and final inspection. A part that fits a press envelope can still need a different layout or forming route.
Blank layout and material flow
Review the unfolded shape, grain direction and how material enters each formed feature. Nesting alone does not establish a stable strip layout; carriers, pilots, feed clearance and the release sequence also matter.
Radii, walls and forming depth
Review inside radii and transitions against alloy, temper and thickness. Deeper features may need several stages. Wall slope, draw direction, thinning and springback must be evaluated together rather than applying one universal radius or draft rule.
Holes, slots and nearby bends
Identify features that must remain round or aligned after forming. Their distance from a bend or drawn wall can affect distortion and process order. Specify functional location controls and discuss whether a feature should be made before or after forming.
Burrs, edges and contact surfaces
State permitted burr direction, edge condition and any contact or handling surfaces. Blanking and piercing create sheared edges; deburring or another operation may be needed. Show cosmetic faces and areas where tool marks are restricted.
Spring behavior and final condition
For clips and contact parts, distinguish dimensional acceptance from the required force or electrical function. Define any functional test, heat treatment and plating condition. Agree which requirements apply to the finished part.
Resolve the functional features before committing to the tool.
Share the critical fits, material condition and expected demand. The quotation can then separate tool development, validation and production.
CAD + material + thickness + quantitySpecify the grade, temper and supply condition.
A metal name and thickness do not establish stampability. Formability, strength, surface requirements and the final part function must be considered together.
| Material group | Identify in the drawing | Manufacturing consideration |
|---|---|---|
| Carbon and low-alloy steels | Grade, strength class, thickness tolerance and coating. | Confirm ductility, forming sequence, corrosion protection and edge condition. |
| Stainless steels | Exact alloy, temper, surface finish and grain direction. | Review work hardening, springback, surface marking and any post-form treatment. |
| Aluminum alloys | Alloy and temper, including any treatment before or after forming. | Forming behavior varies with temper and geometry. Confirm radii, surface protection and final condition. |
| Copper and brass alloys | Exact grade, temper, conductivity and contact-face requirements. | Review bend severity, elastic behavior, burr direction and any plating sequence. |
Provide the specified sheet or strip standard and material documentation requirements. Availability and suitability are confirmed for the quoted part.
Compare the complete cost of the route.
Stamping economics depend on tool investment, design stability and demand over time. Separate the initial tooling decision from the price of a repeat batch.
| Decision | Laser cutting + bending | Dedicated stamping tooling |
|---|---|---|
| Design still changing | Review for early geometry and assembly validation with fewer dedicated tooling commitments. | Freeze important features before committing to tooling; later changes may require tool modification. |
| Repeat demand | Compare setup and processing costs at the planned batch quantities. | Assess tool investment against stable demand, yield, cycle requirements and maintenance. |
| Formed geometry | Press-brake access and bend sequence govern suitability. | Dedicated forming may suit repeated features; material flow and tool feasibility still govern the route. |
| Supplier comparison | Include cutting, bending, finishing and inspection in the scope. | Separate tool charges, sample iterations, part price, maintenance and any secondary operations. |
Agree the tooling terms.
Clarify ownership, storage, maintenance responsibility, expected demand and the treatment of tool changes. For an existing die, provide condition records, drawings and transfer requirements so compatibility can be reviewed.
Agree the approval gate.
Define sample quantity, first-article records, dimensional and functional acceptance, and who approves changes. Manufacturing and tooling schedules are confirmed after review; quote response time is a separate stage.
Define acceptance for the finished part.
Critical dimensions require a datum scheme, units and an agreed measurement condition. Forming angle, hole location and overall size are separate controls.
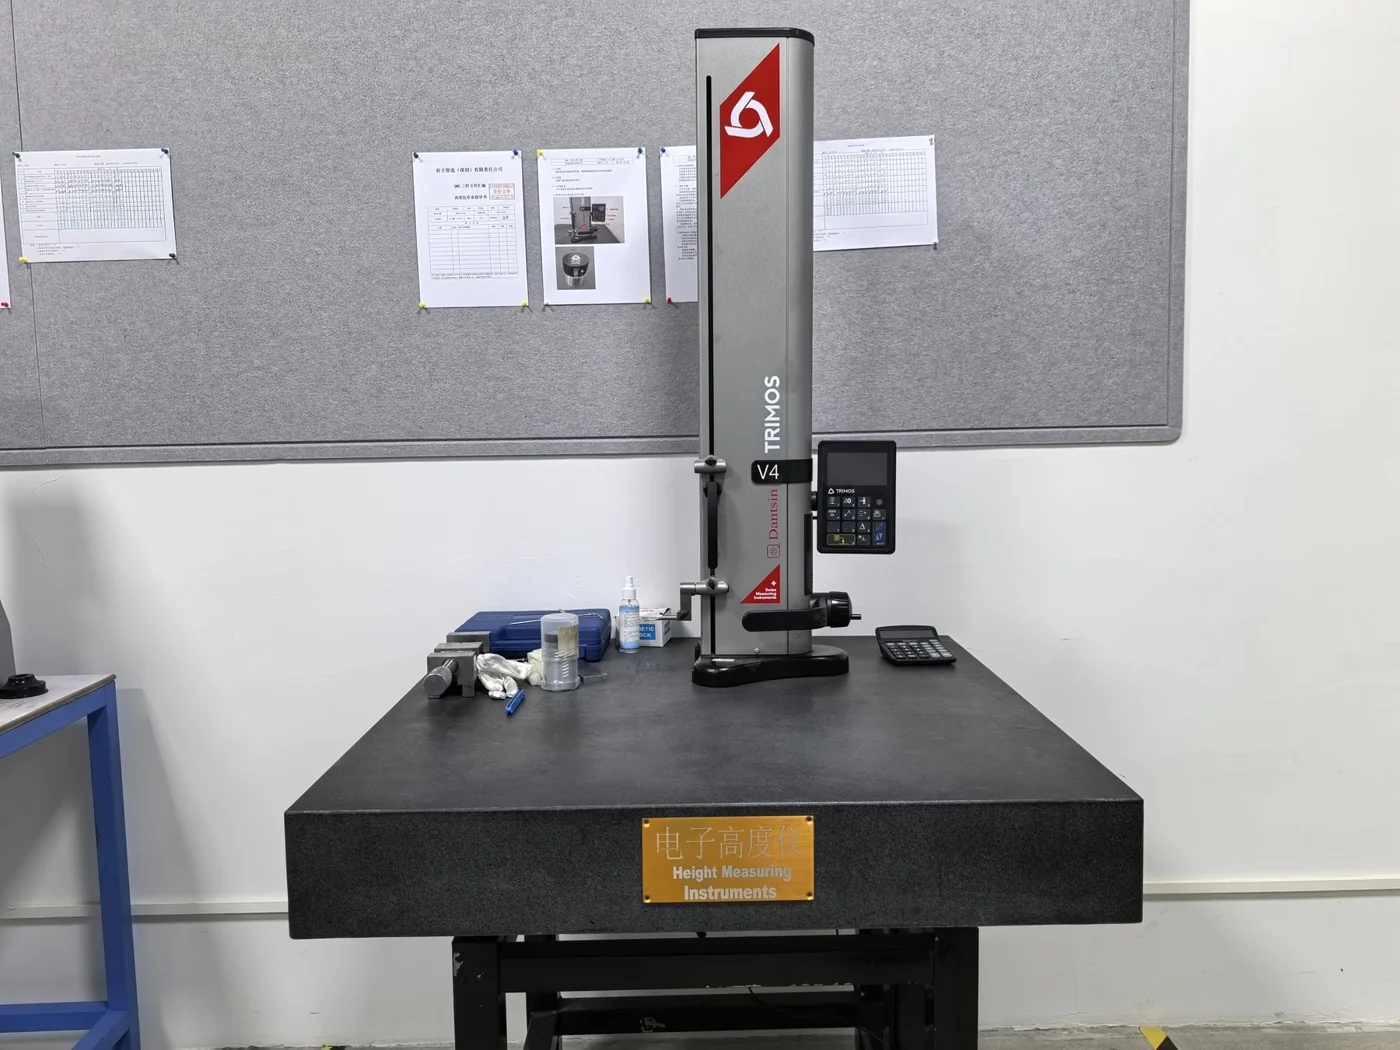

Approve the first article before the repeat run.
Connect the controlled drawing to an agreed inspection plan. Identify the features that govern function and the records required with the finished parts.
- Trial samples and controlled first-article requirements
- Functional contact geometry, material temper and burr direction
- Critical dimensions and the final plating / treatment condition
- Approved tooling changes before repeat production
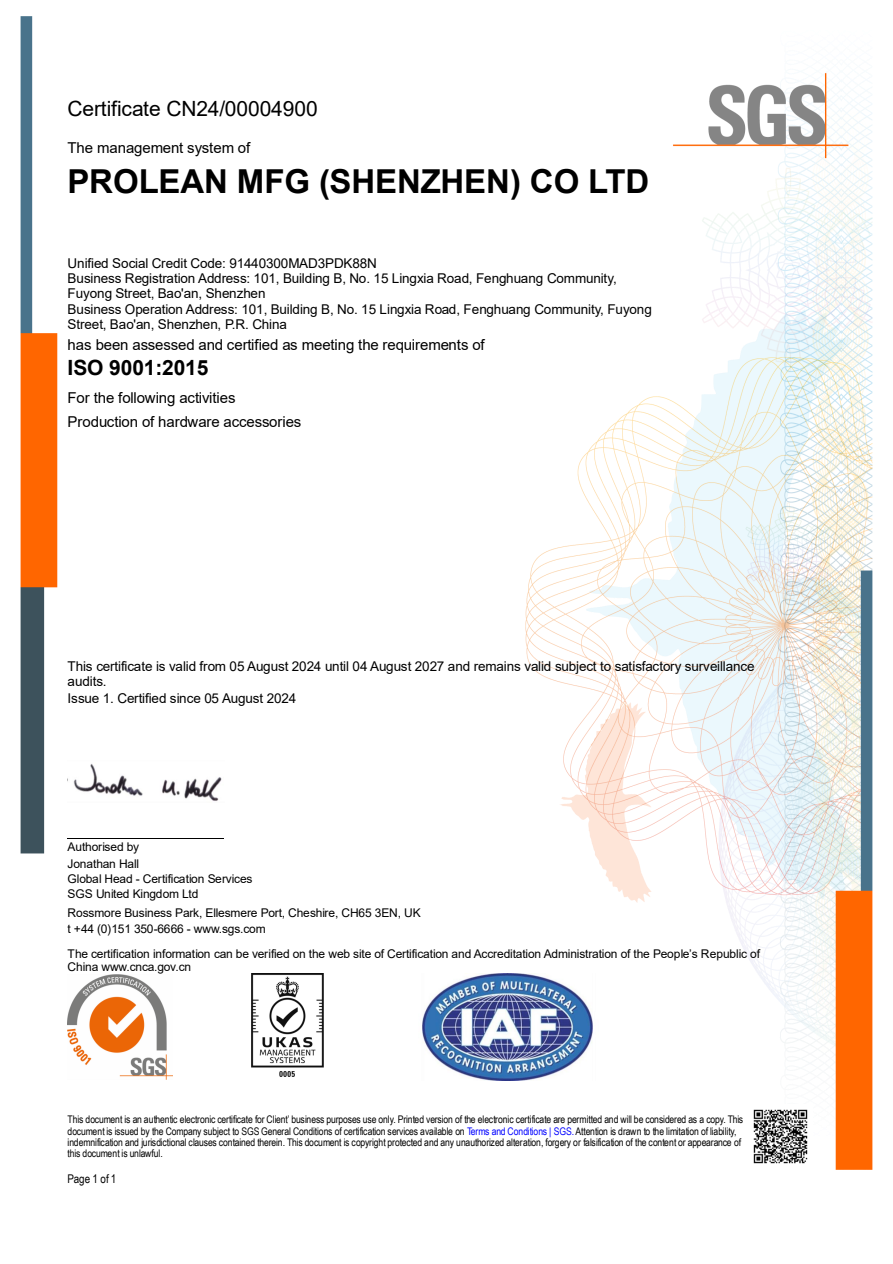
ISO 9001:2015
PROLEAN MFG (SHENZHEN) CO LTD
SGS CN24/00004900
Production of hardware accessories
Quote the tool, first article and repeat production together.
Provide the design, material condition, approval requirements and forecast demand. Separate tooling validation from the production commitment.
Drawing revision + final-state requirements + inspection scopeFrom drawing review to an approved production route.
Send the information that connects the tool decision with the order: CAD and drawing, material condition, batch quantity, annual demand, existing tool status, finish and acceptance requirements.
Share the part and demand.
Include current and expected repeat quantities, design maturity, target dates and any tool-transfer proposal.
Resolve the process and cost.
Review manufacturability, the proposed tooling route, secondary operations, documentation and separate tooling and part charges.
Approve samples and changes.
Agree trial scope, first-article acceptance, permitted adjustments and the release needed before a production batch.
Control the repeat order.
Reconfirm drawing revision, material condition, demand and inspection scope when placing later batches.
Questions before commissioning a die.
Use the drawing and expected demand to establish the next step.
Is stamping suitable for prototypes or a small batch?
Sometimes, but dedicated tooling can dominate the cost. For early designs or uncertain demand, review laser cutting, bending or a suitable pilot tooling approach first. The decision depends on geometry, validation needs and expected repeat orders.
Can I use an existing stamping die?
Provide die drawings, ownership and transfer details, maintenance history, sample parts and known issues. Press compatibility, handling, safety requirements and the tool condition must be reviewed before a production commitment.
Which stamping process is best for my part?
Review feature sequence, forming depth, material flow and quantity together. Progressive, transfer, drawing and multi-direction forming describe different routes. The selected process and available configuration are confirmed for the actual part.
What tolerances should I put on the drawing?
Apply tight controls to functional features with clear datums and units. Distinguish linear dimensions, geometric controls and angles. There is no single tolerance that represents every stamped material, geometry and finishing sequence.
Does a stamping quote include tooling and finishing?
Ask for the scope to be itemized. Identify tool design and build, sample iterations, production parts, finishing, inspection, packaging and freight as applicable. Tool ownership and maintenance terms should be agreed explicitly.
What information helps establish a delivery schedule?
Supply the approved revision, material specification, tool status, quantity, required records and target date. Distinguish tool development, sample approval and batch production; finishing and shipping add separate stages.
Explore the process before the RFQ.
Read these guides alongside your drawing, then confirm the part-specific route with the team.
Metal stamping fundamentals ↗
Cutting, forming and the role of dedicated tooling.
Progressive stamping ↗
How strip-fed operations combine across stations.
Deep drawing ↗
Forming depth, material flow and tooling considerations.
Sheet metal design guide ↗
Connect geometry, material choice and manufacturing decisions.