Custom metal & plastic parts

CNC milling
services.

Pockets, faces, holes and contours. Custom milled metal and plastic parts, from a functional prototype to repeat production.

Bring the drawing. We’ll review cutter access, datums, workholding and critical fits before confirming the manufacturing route.

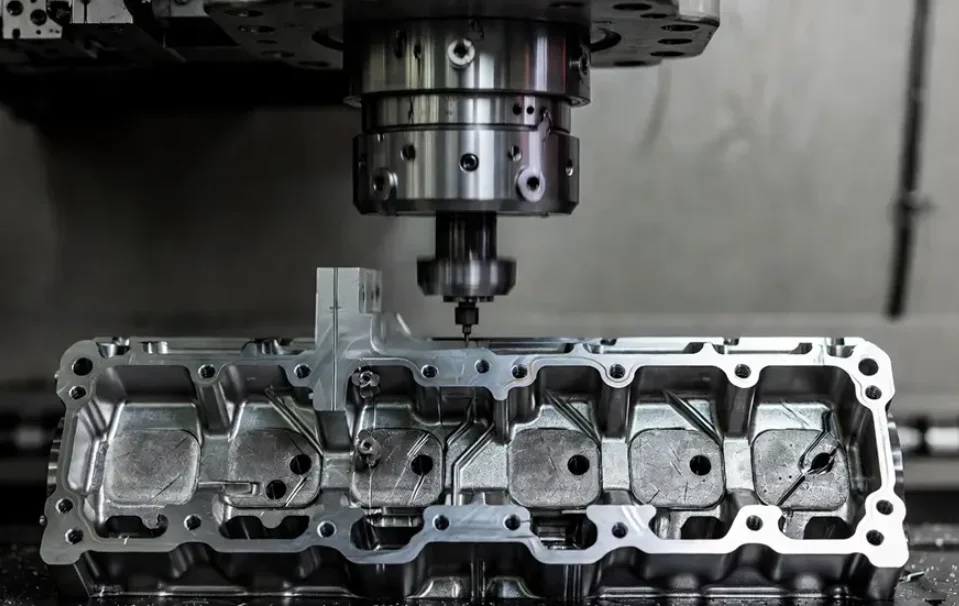
Spindle and cutting tool above a metal component with open cavities and machined faces01 / THE PROCESS
From drawing to partOpen cavities. Clear tool access.
PROCESSES3-axis · 4-axis · 5-axis review
MATERIALSMetals & engineering plastics
ORDER STAGESPrototype → Repeat batches
ACCEPTANCEDatums · fits · inspection

01 / From solid stock to functional geometry

Designed around
the faces that matter.

CNC milling uses a rotating cutter to remove material from a clamped workpiece. It creates pockets, slots, mounting faces, bores and three-dimensional contours for housings, plates, brackets and fixtures.

The number of axes is a routing decision. Start with the faces that must relate to each other, the tool approach and the surfaces available for clamping. A simple part may use several setups; an angled feature may justify indexed or multi-axis access.

Review your milling design ↓

02 / Milling route selection

Choose access.
Then choose the axes.

Select the simplest practical route that can reach the features, hold the part securely and preserve the relationships defined by the drawing.

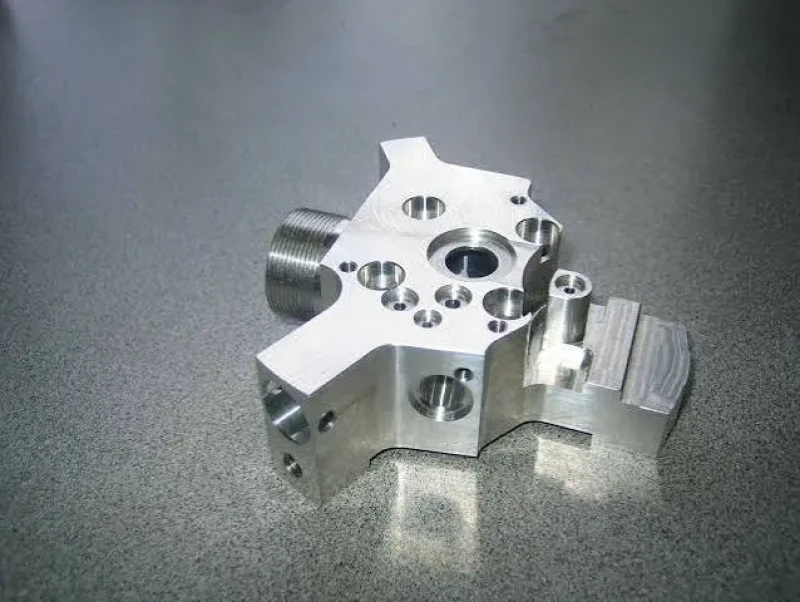
Metal component with machined pockets, bores and flat mounting surfaces01 / FACES & POCKETS

3-axis milling

A fixed tool orientation suits open pockets, flat faces and holes reached from one direction. Other sides may need the part to be reclamped.

Best starting point
Plates, open housings, brackets and fixtures.
Setup check
Keep locating faces consistent across flips; identify relationships between holes and mating faces.
Define the requirements ↓
INDEX TO FACEROTARY AXIS02 / ROTARY ACCESS · ILLUSTRATION

4-axis milling

A rotary axis can present additional faces to the cutter. Indexed machining and cutting while rotating are different strategies; confirm the route for the drawing.

Useful geometry
Features around a part, side holes and repeated faces.
Setup check
Leave space for the fixture and cutter; a rotary axis does not remove access or clamping limits.
Define the requirements ↓
TOOL ORIENTATION / ACCESS03 / ANGLED ACCESS · ILLUSTRATION

5-axis milling

Two rotary degrees of freedom can orient the tool toward inclined features or contoured surfaces. Review 3+2 positioning versus simultaneous motion for the actual geometry.

Useful geometry
Compound angles, multi-face features and freeform surfaces.
Setup check
Confirm machine mode, reach and datum transfer. Five axes do not guarantee one setup or a tighter tolerance.
Define the requirements ↓

03 / Specifications & acceptance

Specify relationships.
Not just dimensions.

Use a controlled drawing to identify critical features. Confirm individual tolerances against geometry, material, workholding and measurement requirements.

Milled-part RFQ and acceptance checklist
RequirementSpecify in the RFQManufacturing implication
Stock & finished envelopeOverall X/Y/Z, stock condition, deep features and accessible clamping faces.Travel alone does not establish usable capacity; tools and fixtures also need clearance.
Datums & geometric controlsPrimary, secondary and tertiary datums; flatness, position and perpendicularity where functional.Links setup and inspection to the way the part locates in assembly.
Pockets, slots & wallsDepths, internal radii, minimum wall sections and any undercuts.Reveals cutter reach, rigidity and possible special operations.
Bores, holes & threadsDiameter limits or fit, hole position, thread standard/pitch and full usable depth; blind or through.Separates thread engagement from drilling and tool runout space.
Surface & edge acceptanceRa on functional faces, cosmetic zones, edge breaks and burr restrictions at intersections.Defines sealing, appearance and assembly requirements beyond dimensions.
Final condition & recordsDimensions after coating, masked bores, material condition, inspection method and report scope.Prevents a machined fit from being changed by finishing or heat treatment.
i

Resolve drawing notes before cutting. State units, revision and the complete general tolerance standard and class. Identify which dimensions apply after heat treatment or finishing, and how flexible parts should be supported during measurement.

04 / Materials for milled parts

Select the grade.
Plan the stock removal.

A process-appropriate shortlist for milling. Grade, condition, geometry and required documentation are reviewed for each quote; this list does not indicate stocked inventory.

Material library ↗
AL / METAL

Aluminum

6061 · 7075

Housings, plates and fixtures where weight matters. Pocketing and uneven stock removal can release stress in thin sections.

Review for millingAlloy / temper · flatness · anodizing zones
FE / METAL

Stainless steel

303 · 304 · 316L · 17-4PH

Corrosion-resistant brackets and housings. Grade and condition change machinability, cutting load and finishing choices.

Review for millingGrade / condition · passivation · mating faces
FE / METAL

Carbon & alloy steel

1018 · 1045 · 4140

Fixtures, loaded brackets and wear interfaces. Plan machining, heat treatment and final inspection in the right sequence.

Review for millingHardness · heat treatment · protective finish
CU / METAL

Brass & copper

H62 brass · C110 copper

Milled conductive blocks, terminals and thermal interfaces. Distinguish the exact alloy and functional surface needs.

Review for millingAlloy · contact surfaces · burr limits
POM / PLASTIC

POM / acetal

Exact grade to review

Milled guides, insulating fixtures and low-friction components. Check clamping distortion and the conditions used to inspect fits.

Review for millingGrade · fit · temperature at inspection
PA / PEEK / PLASTIC

Nylon & PEEK

Unfilled / filled grade to review

Nylon needs moisture-aware dimensional planning; PEEK selection depends on temperature, chemistry and filler content.

Review for millingPolymer / fillers · conditioning · environment

Material grades, condition and availability are reviewed for each quotation.

05 / Finishing milled geometry

Protect the surface.
Preserve the fit.

Finishing follows the function of each face. Map cosmetic zones, mating features and masked areas on the drawing before the route is quoted.

Explore surface finishing ↗
01

As-machined & deburred

Specify functional roughness where needed and acceptable cutter marks on other faces. Define edge breaks and inspect intersecting holes for burrs; “deburr” alone does not define a cosmetic finish.

02

Bead blasting & anodizing

For aluminum parts, agree texture, color reference and cosmetic zones. Anodizing can change mating dimensions; define masking on bores, threads and electrical contact faces.

03

Passivation, plating & coatings

Choose a treatment compatible with the alloy and environment. Confirm thickness, coverage and the final acceptance condition; narrow pockets and hidden faces may need special review.

04

Polishing & functional interfaces

Identify sealing or thermal contact faces separately from visible exterior faces. Agree texture direction and avoid removing material from controlled fits without allowance.

06 / Quality & inspection

Make the requirements clear.
Make the checks meaningful.

For milled parts, agree how bores, mounting faces and pocket features are located from the drawing datums. Confirm access for measurement as well as access for cutting.

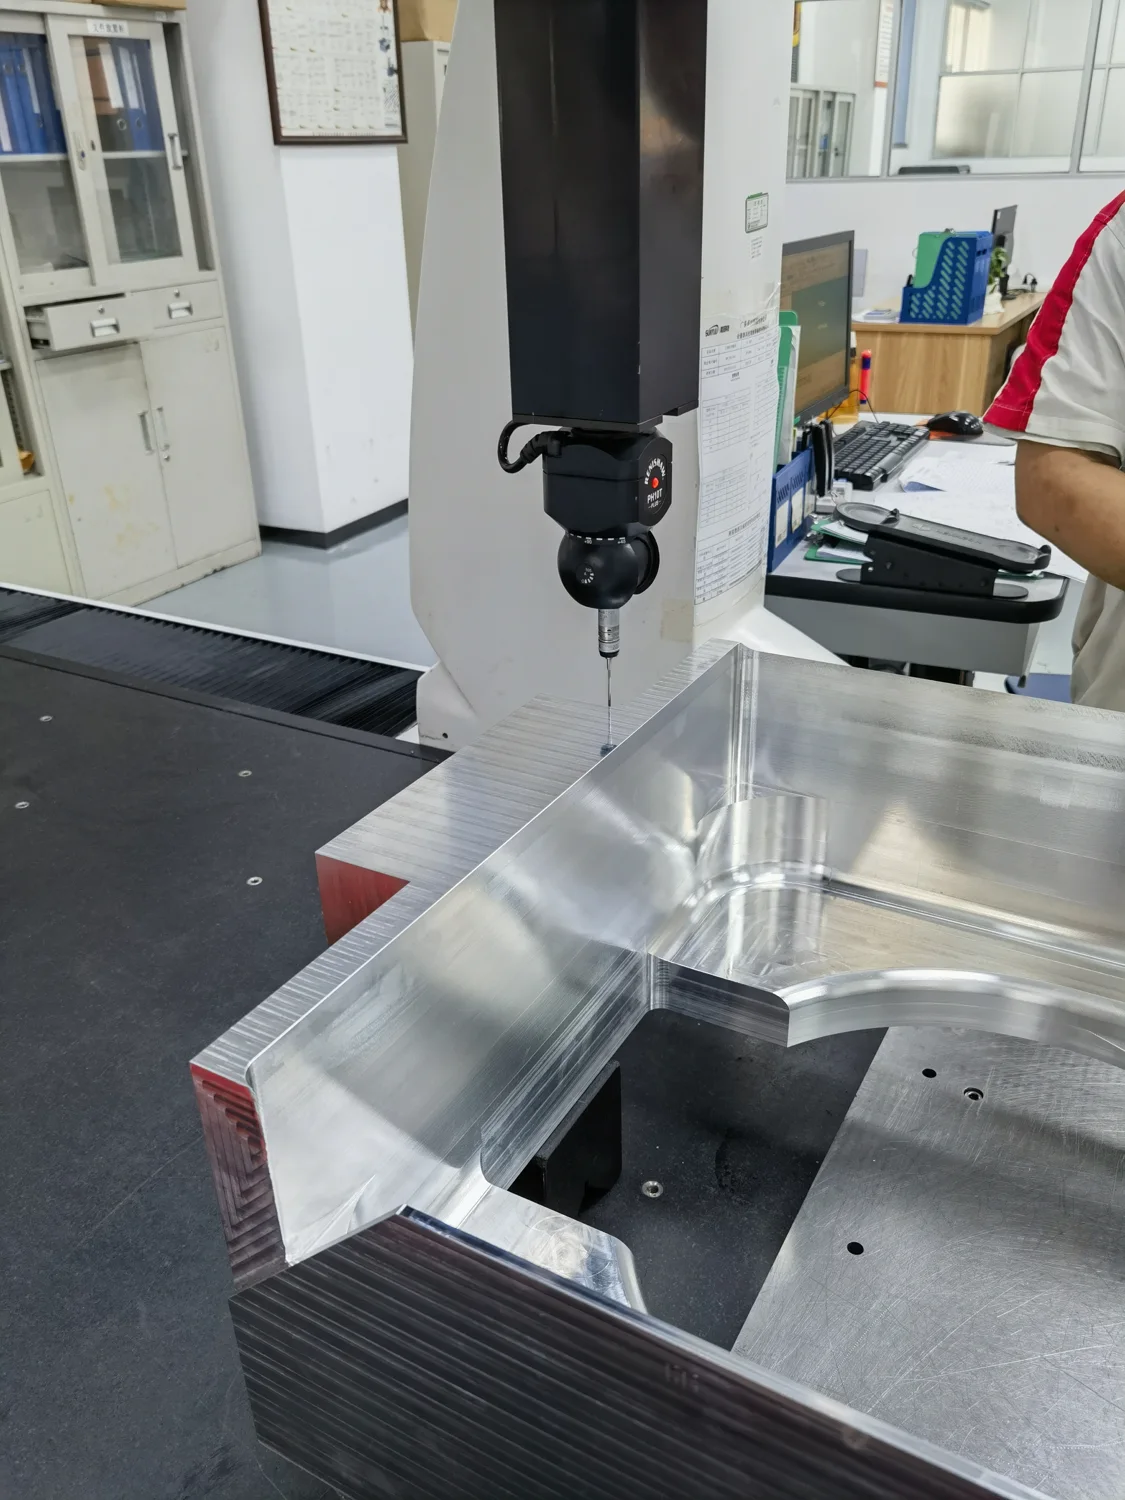
Touch probe measuring features on a machined metal part
Dimensional inspectionCheck the feature. Reference the drawing.
  1. 01

    Agree the acceptance plan

    Confirm the revision, datum setup, critical bore positions and flatness requirements. Define whether checks apply in the free state or with agreed support for thin parts.

  2. 02

    Match the check to the characteristic

    Use an appropriate dimensional method for hole position, face relationships and pocket geometry. Define thread gauging and surface checks separately; a dimensional report does not establish material composition or hardness.

  3. 03

    Define the records you need

    Identify critical features for first-article review and any batch sampling, material records or post-finish reports needed. Confirm document scope and traceability in the quotation.

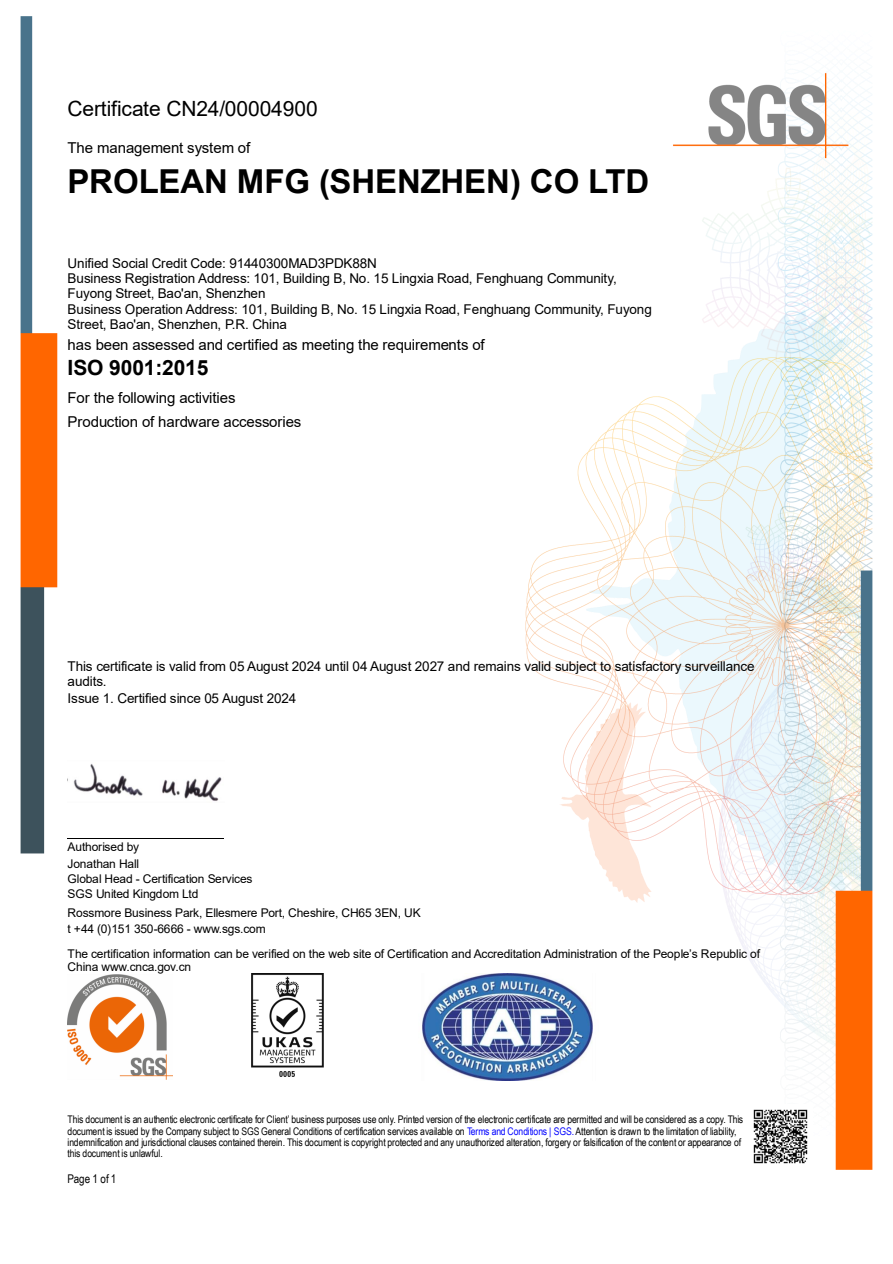
SGS ISO 9001:2015 certificate for PROLEAN MFG (SHENZHEN) CO LTD
Documented quality management

ISO 9001:2015

PROLEAN MFG (SHENZHEN) CO LTD
SGS · CN24/00004900

Scope: Production of hardware accessories.
View original certificate ↗

Certificate dates: 05 Aug 2024–04 Aug 2027, subject to satisfactory surveillance audits. Certification concerns the management system; part acceptance follows the agreed specification.

Explore our quality & inspection approach ↗

07 / Milling DFM & cost guidance

Resolve the details
before they become rework.

These design checks help prepare a useful manufacturing conversation. Final dimensions and process decisions depend on the part’s function and geometry.

Milling DFM illustration: plan view pocket radius and bore, section view cutter reach, thin floor and clamping datumsR / CORNER ACCESSBORE / FITPLAN VIEWWALLDEPTHA / LOCATING FACESECTION / TOOL REACHFLOORDesign review / illustrative geometry

Function → feature → process → inspection.

Internal radii & cutter clearance

A round end mill leaves a radius in an internal plan-view corner. Give the cutter room to move through the corner; where function permits, a larger radius lets a more rigid tool reach the pocket. If a square mating part must seat, consider a relief feature or review a separate process rather than specifying a zero-radius milled corner.

Deep cavities & narrow slots

Review depth together with opening width, corner radius and holder clearance. Long tool overhang reduces rigidity and makes chip evacuation more difficult. Consider a wider opening, shallower pocket or split assembly where function allows; confirm any undercut and special tool access explicitly.

Thin walls & floors

Tall walls and broad thin floors can deflect under cutting and clamping loads. Provide uniform sections and support where possible. Roughing sequence, residual stress and unclamping can affect final flatness, so agree the free-state requirement and inspection support before choosing a route.

Workholding, datums & multiple setups

Reserve accessible clamping and locating faces. Use assembly function to define primary, secondary and tertiary datums, then identify features whose relationships cross setups. Discuss sacrificial tabs or extra stock before changing the model; reorienting the part does not preserve datum relationships automatically.

Holes, threads & intersecting features

Prefer standard hole and thread sizes where function allows. Specify through/blind condition, full usable thread depth, drill depth and any bottom clearance separately. Identify inserts, cross holes and burr-sensitive intersections; avoid demanding full threads to the floor of a blind hole without tool runout space.

Cost, finish & inspection priorities

Cost follows stock volume removed, tool reach, setups, tight features, finishing, inspection and batch size. Keep tight controls on functional faces, combine accessible features where practical and quote quantity breaks. Mark dimensions after coating and masking needs; a more complex axis route is justified only when the geometry and total process support it.

08 / Parts & applications

The application
changes the questions.

Typical milled-part geometries and the requirements they raise. These examples are design references, without customer attribution or application-specific qualification claims.

Automation & robotics

Mounting plates
& brackets

Relate hole patterns and locating bores to the mounting face. Review flatness after unclamping and access to side features.

Define early
Datum scheme · fit · wear surfaces
Robotics applications ↗
Thermal & fluid systems

Pocketed housings
& manifold blocks

Review channel access, sealing lands and intersecting passages. Specify leak or pressure testing separately if required; it is not implied by milling.

Define early
Sealing faces · ports · test requirements
Liquid cooling applications ↗
Product development

Fixtures, covers
& prototype bodies

Check locating faces, insert positions and the walls left after pocketing. Identify whether the prototype must prove assembly, stiffness or thermal behavior.

Define early
Test purpose · drawing revision · volume
Prototyping services ↗

For regulated or safety-critical applications, provide the applicable standards, traceability and validation requirements. Project suitability and documentation require specific review.

09 / Prototype to production

A clear path from
RFQ to repeat order.

Prototype and repeat milling need a controlled revision and an agreed setup plan. Share current quantities, likely repeat demand and any first-article approval gate.

  1. 01 / SHARE

    Send the requirements

    Send CAD and a drawing with datum faces, pocket depths, usable threads, material condition and finish. Include quantities, inspection records and your target date.

  2. 02 / REVIEW

    Resolve the details

    Resolve tool reach, clamping access, datum transfer and finish allowances. Confirm price, documentation and manufacturing lead time for the agreed route.

  3. 03 / CONFIRM

    Align before cutting

    Freeze the revision and acceptance plan. Agree sample or first-article approval, material requirements and any finishing masks before machining starts.

  4. 04 / DELIVER

    Inspect & plan the next run

    Complete agreed dimensional and surface checks. Protect machined edges and faces in packaging. For repeats, reconfirm revision, stock condition and changed demand.

For procurement teams

Ask for pricing at your planned quantities and clarify material documents, inspection scope, packaging, freight and delivery terms. This makes supplier comparisons more useful than a unit price alone.

10 / CNC milling FAQs

Before you
send the drawing.

Practical answers for engineers,
buyers and manufacturing teams.

Ask a project-specific question ↗
How should I choose 3, 4 or 5-axis milling?

Start with feature access and datum relationships. Open pockets and holes in one direction often suit 3-axis work. Rotary indexing can present side faces; 5-axis orientation can help inclined features and contours. Confirm indexed or simultaneous motion, workholding and measurement for the actual part; extra axes do not guarantee one setup.

Can milling produce sharp internal corners?

A rotating end mill leaves an internal corner radius in plan view. If a square component must seat, show the functional clearance and consider a relief. A truly sharp internal profile may require a different operation, subject to geometry and material review.

What makes a deep pocket expensive?

Depth, a narrow opening and a small corner radius can require a long, slender tool. Reach, chip evacuation, holder clearance and additional finishing passes then become concerns. Widening access or relaxing a nonfunctional radius can be more useful than simply specifying more axes.

How are thin walls and flat plates reviewed?

Review wall height, unsupported area, clamping loads, material condition and stock removal sequence together. Define flatness and the measurement condition. There is no universal minimum wall thickness or flatness guarantee for every geometry.

What must I specify for blind threaded holes?

State thread standard, size, pitch or class, full usable engagement depth and whether the hole is blind. Distinguish usable thread from drill depth and provide bottom clearance for the chosen tool. Identify inserts and intersecting holes that require specific deburring.

What tolerances can be held after finishing?

Mark individual fits and geometric controls, with datums and units. Identify which apply after coating or heat treatment and which features need masking. Feasibility depends on the material, feature, setup and measurement method; the drawing and agreed quotation establish acceptance.

Which files and quantities should I send for a milling quote?

Provide STEP/STP or IGES plus a controlled PDF drawing, exact material and condition, finish and inspection scope. Include prototype and repeat quantity breaks. Confirm any first-article review and NDA before sending confidential files via the agreed channel.

How long will my milled parts take?

Material sourcing, tool access, number of setups, batch size, finishing and inspection all affect the schedule. Share the target date and staged-delivery needs. Quote response time is separate from manufacturing lead time; an order-specific commitment requires review.

Scroll to Top